Decanter centrifuge applications extend across industries where continuous separation of solids from liquids—or, in suitable configurations, separation involving two liquid phases—is required.From wastewater sludge dewatering and food processing to edible oils, fermentation, mining and biofuels, decanter centrifuges help industries recover valuable materials, reduce waste and improve process efficiency.
Alfa Laval decanter centrifuges use centrifugal force for continuous solid-liquid separation and are designed to accommodate varying feed conditions while delivering controlled separation performance.For industries looking for reliable centrifugal separation technology, understanding the different decanter centrifuge applications is an important first step towards selecting the correct equipment.
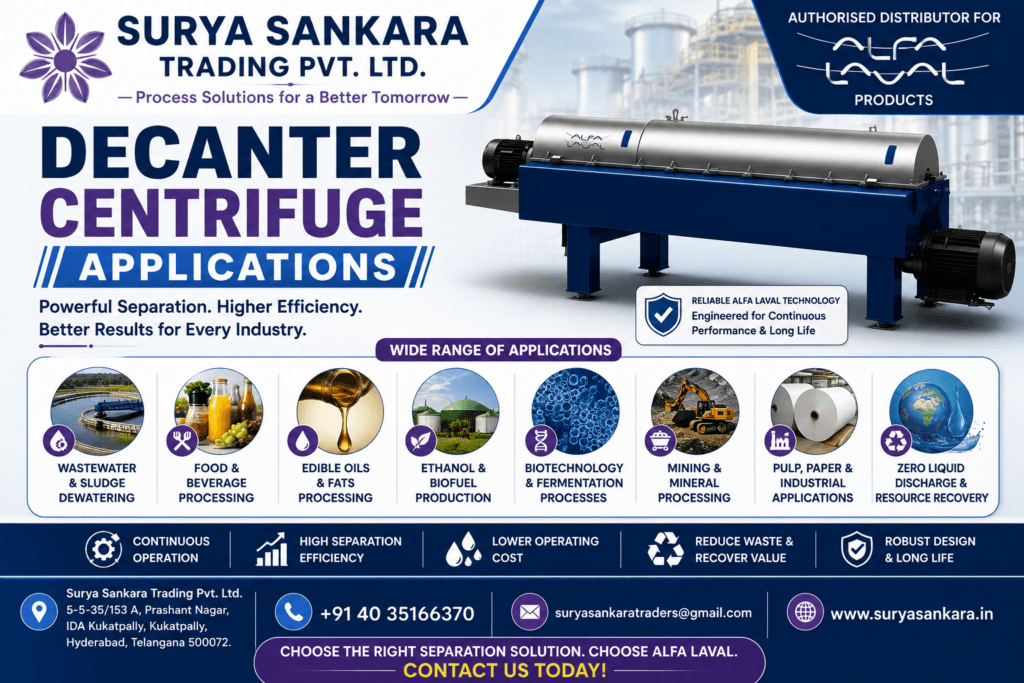
Check out about Decanters:
01) What is decanter centrifuge
02) How does a centrifuge work?
1. Wastewater Treatment and Sludge Dewatering – Decanter Centrifuge Applications
Wastewater treatment is one of the most important applications for industrial decanter centrifuges.
Decanters can be used for:
- Municipal wastewater sludge
- Industrial wastewater treatment
- Sludge thickening
- Sludge dewatering
- Potable water treatment residuals
- Biogas plant sludge
- Solid-waste treatment processes
Removing water from sludge reduces its volume and weight, potentially lowering transportation and disposal requirements.
Alfa Laval’s ALDEC centrifuges, for example, are specifically designed for sludge thickening and dewatering in municipal and industrial wastewater treatment as well as potable-water works, solid-waste plants and biogas plants.
2. Food and Beverage Processing – Decanter Centrifuge Applications
Food processing represents another major category of decanter centrifuge applications.
Depending on the process, decanters can separate solids from liquids or perform multi-phase separation while maintaining continuous production.
Applications include:
- Breweries
- Fruit and vegetable juices
- Coffee and tea processing
- Distilleries
- Plant-based beverages
- Plant proteins
- Starch processing
- Wine production
- Dairy-related processing
- Food oil extraction
Alfa Laval’s Foodec range is designed for food and beverage processing where separation efficiency, hygienic operation and cleaning are important.
3. Edible Oil and Fat Processing – Decanter Centrifuge Applications
Decanter centrifuges play an important role in extracting and recovering oils and fats from different raw materials.
Typical applications include:
- Olive oil processing
- Palm oil processing
- Seed oil production
- Avocado oil
- Fish processing
- Rendering
- Animal protein processing
- Food-related oil recovery
Three-phase decanter technology can be particularly useful when a process requires the separation of oil, water and solids.
Efficient separation can help manufacturers improve product recovery and make better use of valuable raw materials.
4. Ethanol and Biofuel Production
The ethanol and biofuel industries require efficient separation technologies capable of handling continuous production and significant solids loads.
Decanter centrifuges can be used to separate solids and liquids during ethanol production and related biofuel processes.
Alfa Laval’s SG2 decanter range, for example, is designed specifically for dewatering applications in ethanol and biofuel production.
Effective centrifugal separation can contribute to:
- Improved solids recovery
- Continuous processing
- Reduced liquid content in separated solids
- Better utilization of process streams
- Efficient high-volume production
5. Life Science, Biotechnology and Fermentation
Modern biotechnology processes frequently require efficient separation of biomass from fermentation liquids.
Relevant decanter centrifuge applications include:
- Fermentation processes
- Biomass separation
- Protein processing
- Biological process streams
- Recovery of valuable solids
The ability to continuously process feed streams makes decanter centrifuges useful in industrial biotechnology where reliable solids separation is required.
6. Protein and Animal Processing
Decanter centrifuges can also be used for protein recovery and processing.
Typical applications include:
- Fish processing
- Meat processing
- Rendering
- Pet food processing
- Vegetable protein production
- Surimi processing
- Blood processing
- Gelatine production
Depending on the application, valuable fats, oils and proteins can be recovered from the incoming process stream.
7. Mining and Mineral Processing
Mining operations often involve large volumes of slurry containing suspended solids.
Industrial decanter centrifuges can support:
- Mining and tailings treatment
- Mineral exploration drilling
- Slurry treatment
- Solids recovery
- Process-water recovery
- Dewatering applications
Continuous separation can help reduce the volume of material requiring disposal while allowing valuable process liquids to be recovered or reused where appropriate.
8. Oil, Gas, Drilling and Construction
Decanter centrifuges are also used in demanding drilling and construction applications.
Examples include:
- Oil and gas drilling
- Exploration drilling
- Horizontal directional drilling
- Tunnel boring
- Construction-site wastewater
- Drilling-fluid clarification
These applications may involve abrasive solids and demanding operating conditions, making equipment design and wear protection important considerations.
9. Pulp, Paper and Industrial Processes
Decanter centrifuges can support industrial processes where solids must be separated from process liquids continuously.
Applications can include:
- Pulp and paper processing
- Chemical processes
- Industrial effluent treatment
- Process-water recovery
- By-product recovery
- Waste minimization
By separating useful material from process streams, businesses may be able to improve raw-material utilization and reduce the amount of waste requiring further treatment.
10. Zero Liquid Discharge and Resource Recovery
Sustainability and water conservation are increasingly important considerations for industrial facilities.
Decanter centrifuges can form part of separation processes supporting:
- Zero Liquid Discharge (ZLD)
- Water recovery
- Waste-volume reduction
- Solids concentration
- Resource recovery
- Industrial wastewater management
The exact configuration should be determined according to feed composition, solids characteristics, required dryness and downstream treatment requirements.
Why Are Decanter Centrifuges Used Across So Many Industries?
The broad range of decanter centrifuge applications is largely due to their ability to provide continuous centrifugal separation.
Important potential benefits include:
Continuous Operation
The feed can be processed continuously while separated solids are discharged by the internal conveyor.
Efficient Solid-Liquid Separation
High centrifugal forces accelerate sedimentation compared with gravity-based settling.
Reduced Waste Volume
Dewatering can decrease the amount and weight of solids requiring transport, handling or disposal.
Valuable Product Recovery
In certain processes, the separated solid or liquid is a valuable product rather than waste.
Flexible Processing
Operating parameters can be adjusted to accommodate variations in feed and process requirements.
Compact Separation
High centrifugal forces can provide substantial separation capacity within a comparatively compact machine footprint.
How Does an Alfa Laval Decanter Centrifuge Work?
The feed enters a rapidly rotating horizontal bowl.
Centrifugal force causes the denser solid particles to move outward towards the bowl wall. The liquid forms an inner layer, while a screw conveyor rotating at a controlled differential speed transports the deposited solids towards the solids-discharge end.
The separated liquid exits independently.
This continuous operating principle makes the technology suitable for industrial processes requiring reliable handling of substantial volumes of solids and liquids.
How to Select a Decanter Centrifuge for Your Application
The correct decanter should be selected according to the actual process rather than simply machine capacity.
Important factors include:
- Feed flow rate
- Percentage of solids
- Particle size
- Solid density
- Liquid characteristics
- Required cake dryness
- Required liquid clarity
- Abrasiveness of the material
- Product temperature
- Hygiene requirements
- Two-phase or three-phase separation
- Required operating capacity
A detailed evaluation of these parameters can help determine the appropriate centrifuge configuration.
Frequently Asked Questions
What are the most common decanter centrifuge applications?
Common decanter centrifuge applications include wastewater sludge dewatering, food and beverage processing, edible oil extraction, fermentation, biomass separation, ethanol production, mining, drilling and industrial process-water treatment.
What is a decanter centrifuge mainly used for?
A decanter centrifuge is primarily used for continuous separation of solids from liquids using centrifugal force. Suitable designs can also perform three-phase separation.
Can a decanter centrifuge be used for wastewater treatment?
Yes. Decanter centrifuges are widely used for municipal and industrial wastewater sludge thickening and dewatering.
Are decanter centrifuges used in food processing?
Yes. Applications include beverages, plant proteins, starch, wine, brewing, oils, fats and other food-processing operations.
Can a decanter separate oil, water and solids?
Suitable three-phase decanter configurations can separate two liquid phases and a solid phase, making them useful for certain oil and fat processing applications.
What is the difference between a decanter centrifuge and a separator?
A decanter is generally suited to continuous processing of feeds with substantial solids content, while high-speed separators such as disc-stack centrifuges are commonly used for finer clarification and liquid-phase separation.
Industries searching for an Alfa Laval decanter centrifuge in Hyderabad, industrial decanter centrifuge in Telangana, sludge dewatering centrifuge in Hyderabad or centrifugal separation equipment in India can contact Surya Sankara Trading Pvt. Ltd.
As an Authorised Distributor for Alfa Laval products, Surya Sankara Trading supports industrial customers seeking suitable Alfa Laval process and separation solutions.
Find the Right Alfa Laval Decanter for Your Application
Have a Difficult Solid-Liquid Separation Problem? Your feed conditions determine the right decanter—not just the machine specification.
Talk to Surya Sankara Trading Pvt. Ltd., an Authorised Distributor for Alfa Laval products, about your application.
Share your:
Feed material • Flow rate • Solids percentage • Particle characteristics • Required cake dryness • Required liquid clarity • Operating conditions
Our team can help you evaluate the appropriate Alfa Laval decanter centrifuge solution for your industrial separation requirements.
Turn Your Separation Challenge Into a More Efficient Process
Contact Surya Sankara Trading Pvt. Ltd. today for Alfa Laval decanter centrifuge solutions in Hyderabad, Telangana and India.
Request a Consultation | Discuss Your Application | Get the Right Separation Solution